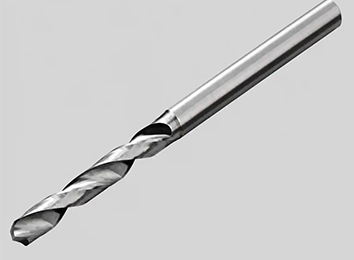
Solid Carbide Through Coolant Drills
Deep holes in steel and stainless steel with better chip clearing, cooler cutting and longer tool life.
Have any questions? Start a conversation with our team.
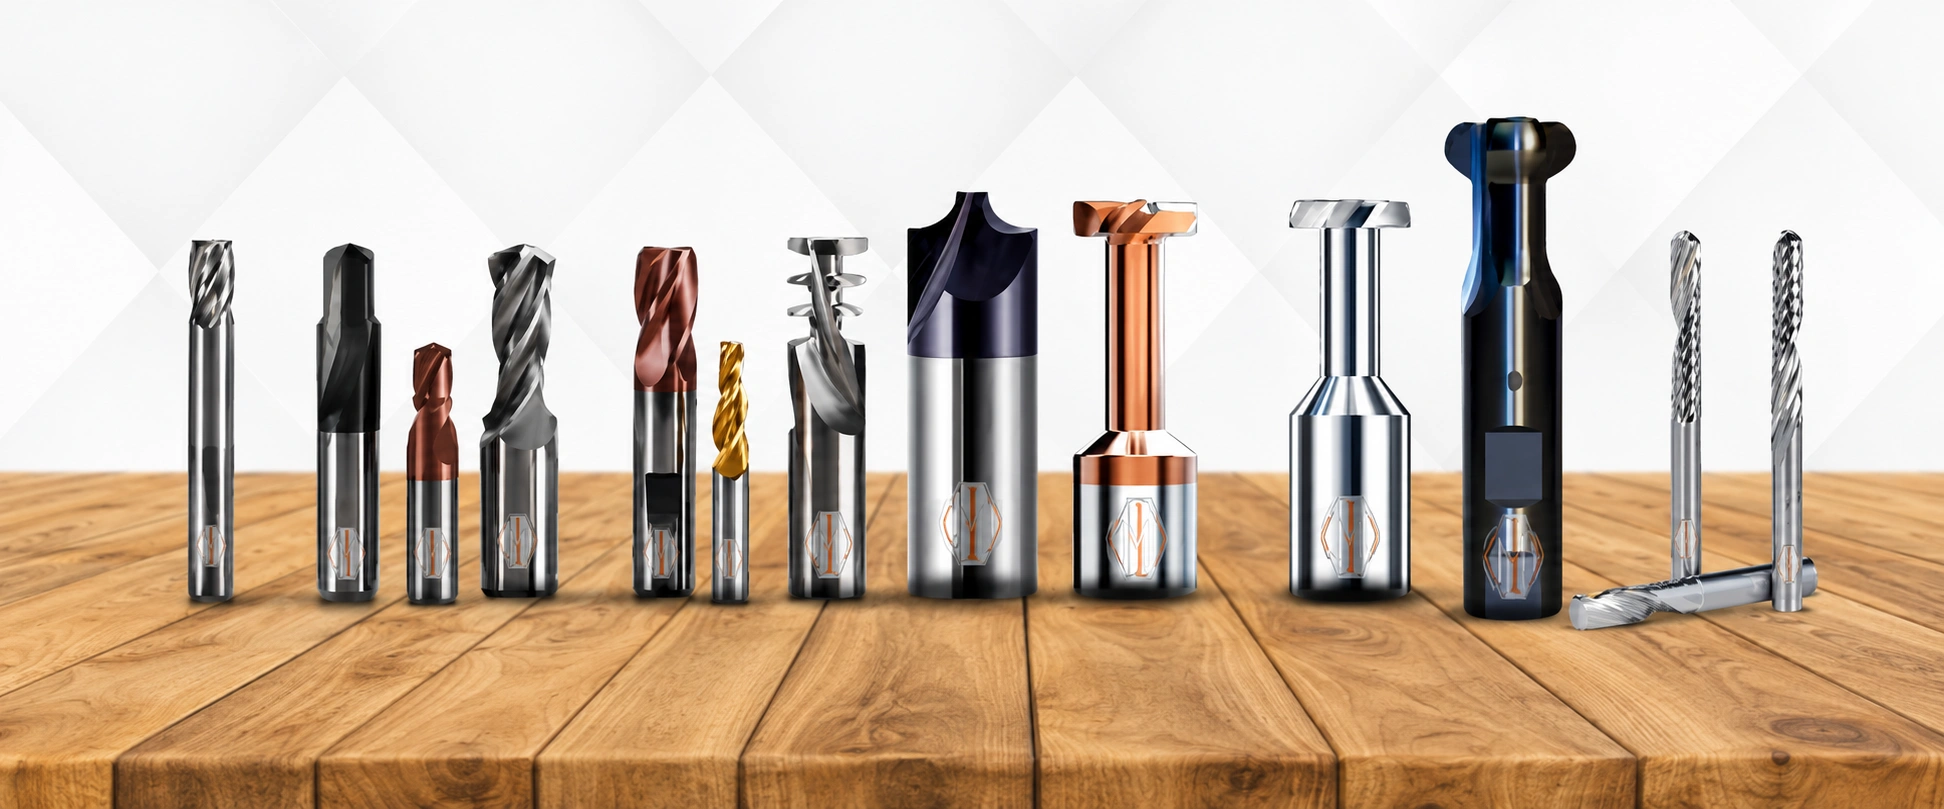
Through-coolant, step, subland and gun drills, precision-made for reliable machining and long tool life. Send us your drawing for a custom solution.
Deep holes in steel and stainless steel with better chip clearing, cooler cutting and longer tool life.
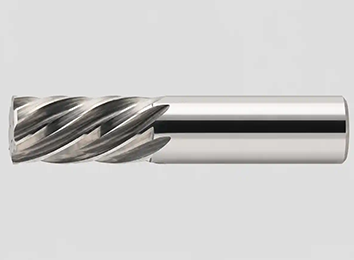
Drill and ream in one pass. One tool, shorter cycle time, accurate hole size.
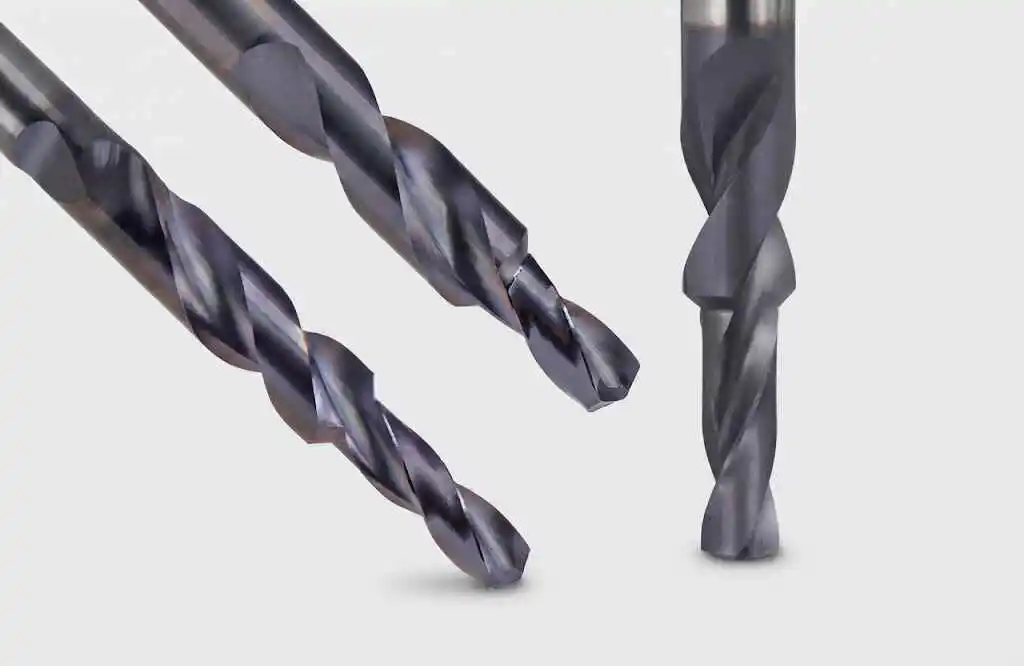
Drill stepped holes in one pass with a clean finish and no extra tool changes.
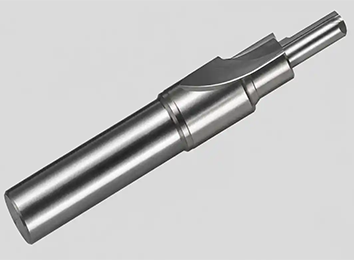
Stable cutting and accurate sizing for precision stepped holes.
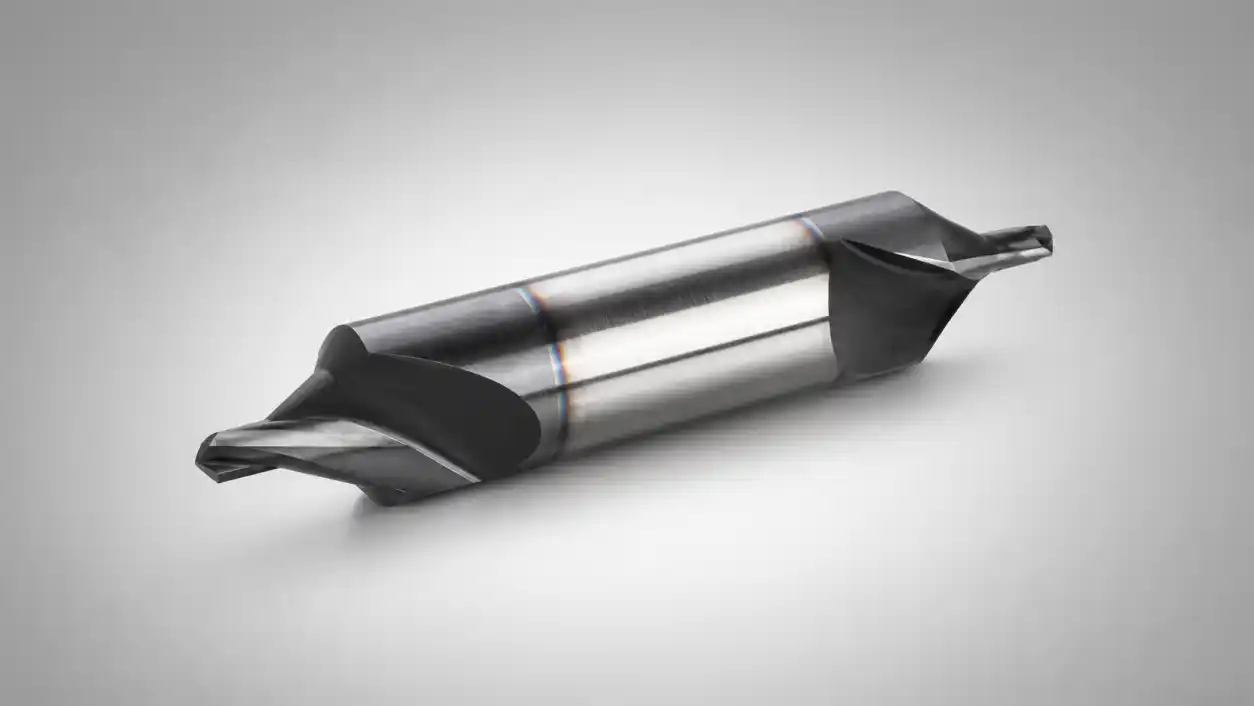
Start every hole in the right place. Less drill walk, better hole position.
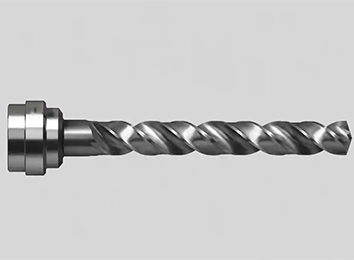
Rigid, heavy-duty drills for tough jobs where stability decides hole quality.
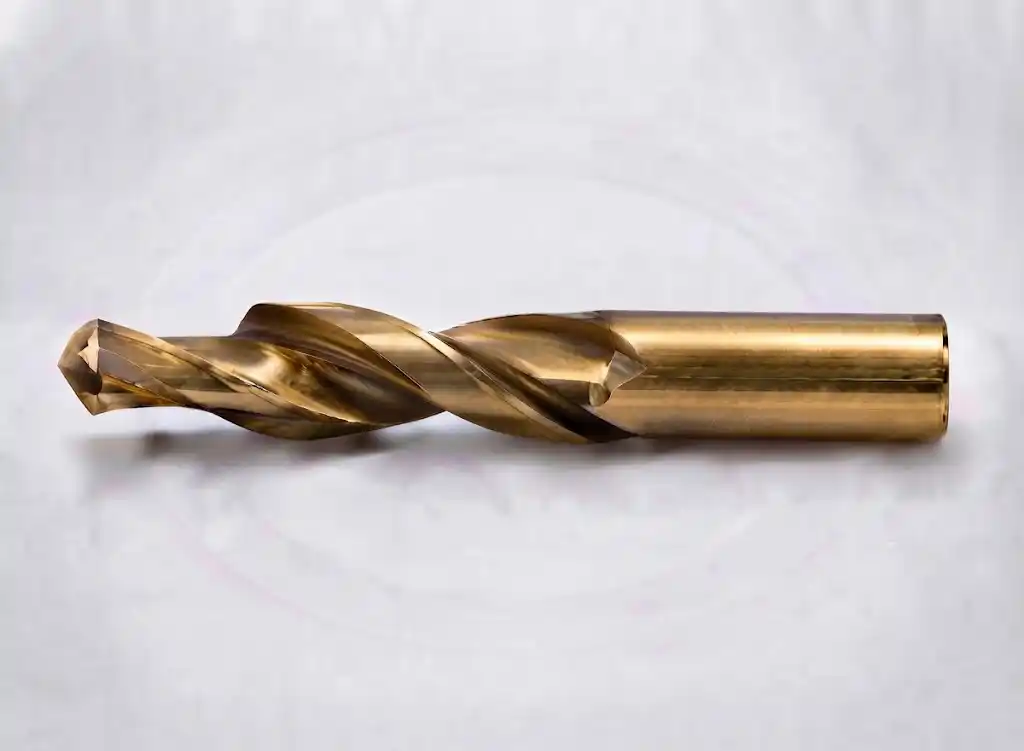
Drill several diameters in one go and cut machining time on multi-step holes.
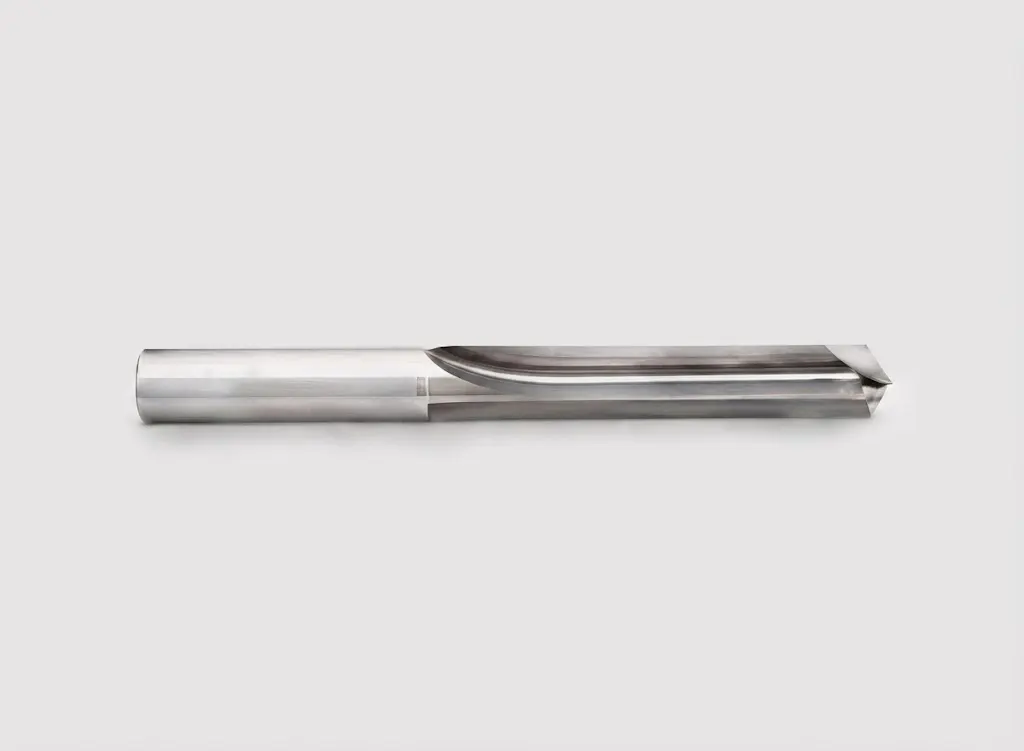
Drill and finish together for a smoother hole surface in a single operation.
Tell us the drill type, diameter and material. Our team replies with your quotation.
For the fastest quote include drill type, diameter, flute and overall length, shank, material, hole depth, coolant and quantity. A drawing helps.
A drill that drifts off size, chips or wears out in the first shift costs more than the tool itself: scrapped parts, machine stops and late deliveries. Mastertech Business Solutions Pvt. Ltd. is a carbide drills manufacturer. We grind every drill on 5-axis CNC machines from premium German carbide rods, so point geometry, flute form and hole size stay repeatable from batch to batch.
The range covers through-coolant, step, straight flute step, subland, burnishing, lugged and center drills, drill cum reamers and gun drills, plus special drills made to your drawing. Automotive, aerospace, defence, railway, turbine and die & mould shops use our tools.
Need a tool beyond drills? See our solid carbide tools, end mills and reamers, or send your drawing for a special drill.
Match the drill to the hole you need to make.
| Job | Recommended drill | Why |
|---|---|---|
| Deep holes | Gun drills, through-coolant drills | Chip evacuation and cooling reach the cutting edge |
| Stepped or chamfered holes | Step drills, straight flute step drills | Two or more diameters in a single pass |
| Several diameters in one go | Subland drills | Fewer tool changes and shorter cycle time |
| Drill and finish together | Drill cum reamer, burnishing drills | Better hole size and surface in one operation |
| Accurate hole start | Center drills | Reduces drill walk and improves position |
| Rigid, heavy-duty jobs | Lugged drills | Stable cutting in demanding applications |
Send your material, hole diameter and depth. We will suggest the right drill and send a quote.
Two questions decide most drill choices: how deep is the hole, and what are you drilling?
| Hole depth | Drill to use | What to know |
|---|---|---|
| Up to about 3×D | Solid carbide drill, drill cum reamer, center drill | External coolant is usually enough. Spot with a center drill first when hole position is critical. |
| About 3×D to 10×D | Through-coolant drill | Coolant reaches the cutting edge and flushes chips out, so pecking can often be reduced or removed. |
| Beyond about 10×D | Gun drill | Built for deep, straight holes. Needs the right coolant supply and a machine set up for deep-hole work. |
D is the drill diameter. These are general guidelines. The right choice also depends on material, machine rigidity and coolant pressure.
Use a through-coolant carbide drill for production runs. Steady feed and good chip clearing give the longest tool life.
It work-hardens when the drill rubs instead of cutting. Keep the feed positive, avoid dwell and flood the cutting edge with coolant.
Abrasive material where carbide wear resistance pays off. Reduce the feed at breakthrough to protect the edge.
Soft, sticky chips can clog the flutes. Choose open, smooth flutes and give plenty of coolant to keep chips moving.
Buy direct from the manufacturer in Pune. A carbide drill costs more per tool, but it usually costs less per hole because it lasts longer and holds size.
Premium German carbide rods hold the point and cutting edges in steel, stainless steel and abrasive cast iron, so you change drills less often.
5-axis CNC grinding keeps point angle, flute form and step diameters the same from one batch to the next.
Stepped, subland, combination or non-standard length drills: share the drawing or a worn sample and we quote the special drill.
Discuss diameter, coolant type, shank and delivery directly with our Pune team.
Our plant is in MIDC Bhosari, close to Pune's industrial belt of Pimpri-Chinchwad, Chakan and Talegaon.
If your machine shop is in or around Pune, talk directly to our team, share your drawing and discuss diameter, coolant type and shank for your job. We make through-coolant, step, subland, burnishing and gun drills in-house, so quotations and delivery schedules are quick to confirm.
One manufacturer, delivering to your plant wherever you are in India.
Send your requirement by phone, WhatsApp or the quote form. We confirm the quotation and the delivery schedule for your location. Buyers outside India can send export enquiries with the country and quantity.
Quick answers to the questions buyers ask us most.
It is a drill whose body and cutting edges are both made from one piece of tungsten carbide, with no brazed tip. The rigid body holds the point geometry under load, so the drill stays on size and runs at speeds that would wear out an HSS drill.
Mastertech Business Solutions Pvt. Ltd. is a carbide drills manufacturer in MIDC Bhosari, Pune, close to the Pimpri-Chinchwad and Chakan industrial belts. We make through-coolant, step, subland, burnishing and gun drills and sell them direct to factories and machine shops, so you speak to the people who grind the tool.
Yes. We dispatch to customers across India. Send your requirement with the location and we confirm the quotation and delivery time.
Yes. We are a manufacturer and exporter. Send the drill type, diameter, quantity and your country, and we will confirm the quotation and shipping details.
For shallow holes in easy materials, a standard drill with external coolant is often enough. Once the hole gets deeper than about three times the diameter, or the material is steel or stainless steel, a through-coolant drill clears chips better and usually lasts longer.
A step drill cuts two or more diameters along one body, often with a chamfer. A subland drill has several lands ground to different diameters, so a multi-step hole is drilled in one pass.
It drills and reams in one stroke, so the hole is opened and brought to size without a second tool. Use it on repeat jobs where a tight hole size and a short cycle time both matter.
The usual causes are poor chip evacuation, low coolant pressure, high runout, a loose setup or the wrong feed at entry and exit. Carbide is hard but brittle, so a rigid setup and correct parameters prevent most breakages.
Yes. We make special drills such as stepped, subland and combination drills, including custom step diameters, chamfers and lengths. Send the drawing or a sample, the material and the quantity for a quotation.
Reamers, end mills and profile tools from the same Pune plant.
Send us the hole you need to drill. Mastertech, a carbide drills manufacturer in Pune, replies with the right drill and a price, and dispatches across India.
Plot No. W-238, J Block, MIDC Bhosari, Anandrao Lande Road, Pune 411026, Maharashtra, India
Send your drill type, diameter and material. Our team will reply with a quotation.
Get a Quote Call +91 9850073333 WhatsApp Us Email Us