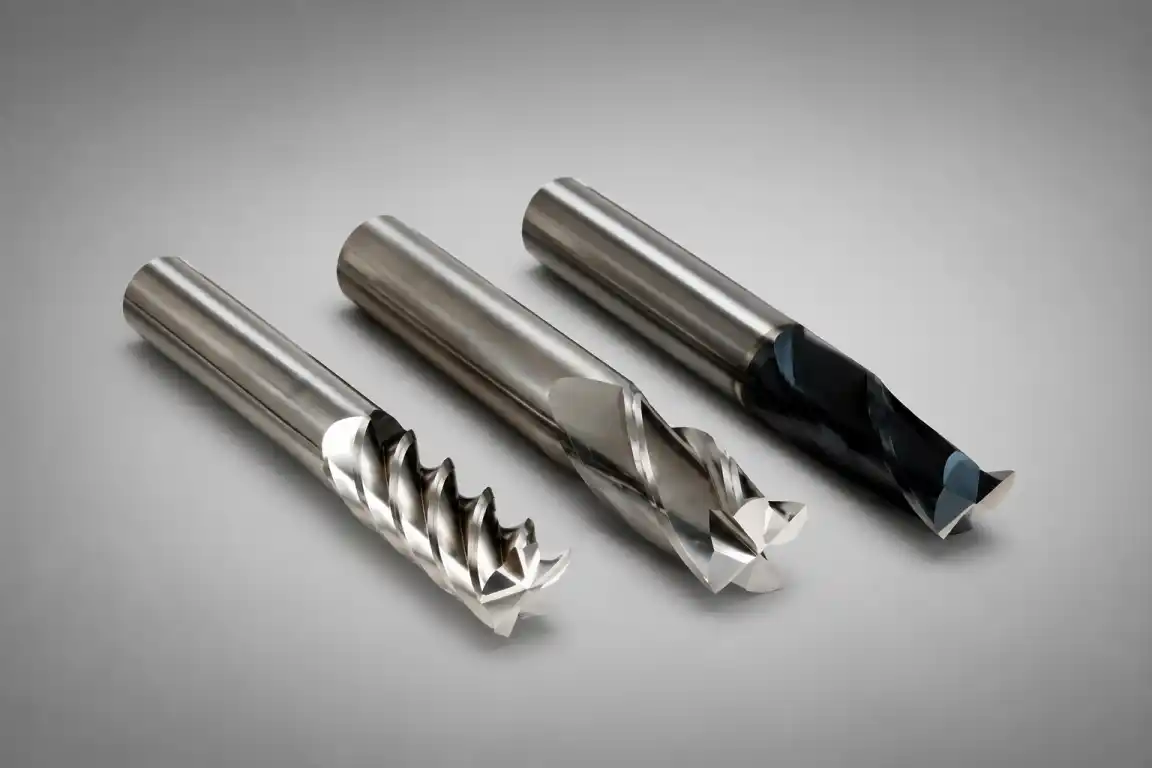
Solid Carbide End Mills
General-purpose end mills for slotting, pocketing, profiling and finishing in steel, stainless steel, cast iron and aluminium.
Have any questions? Start a conversation with our team.
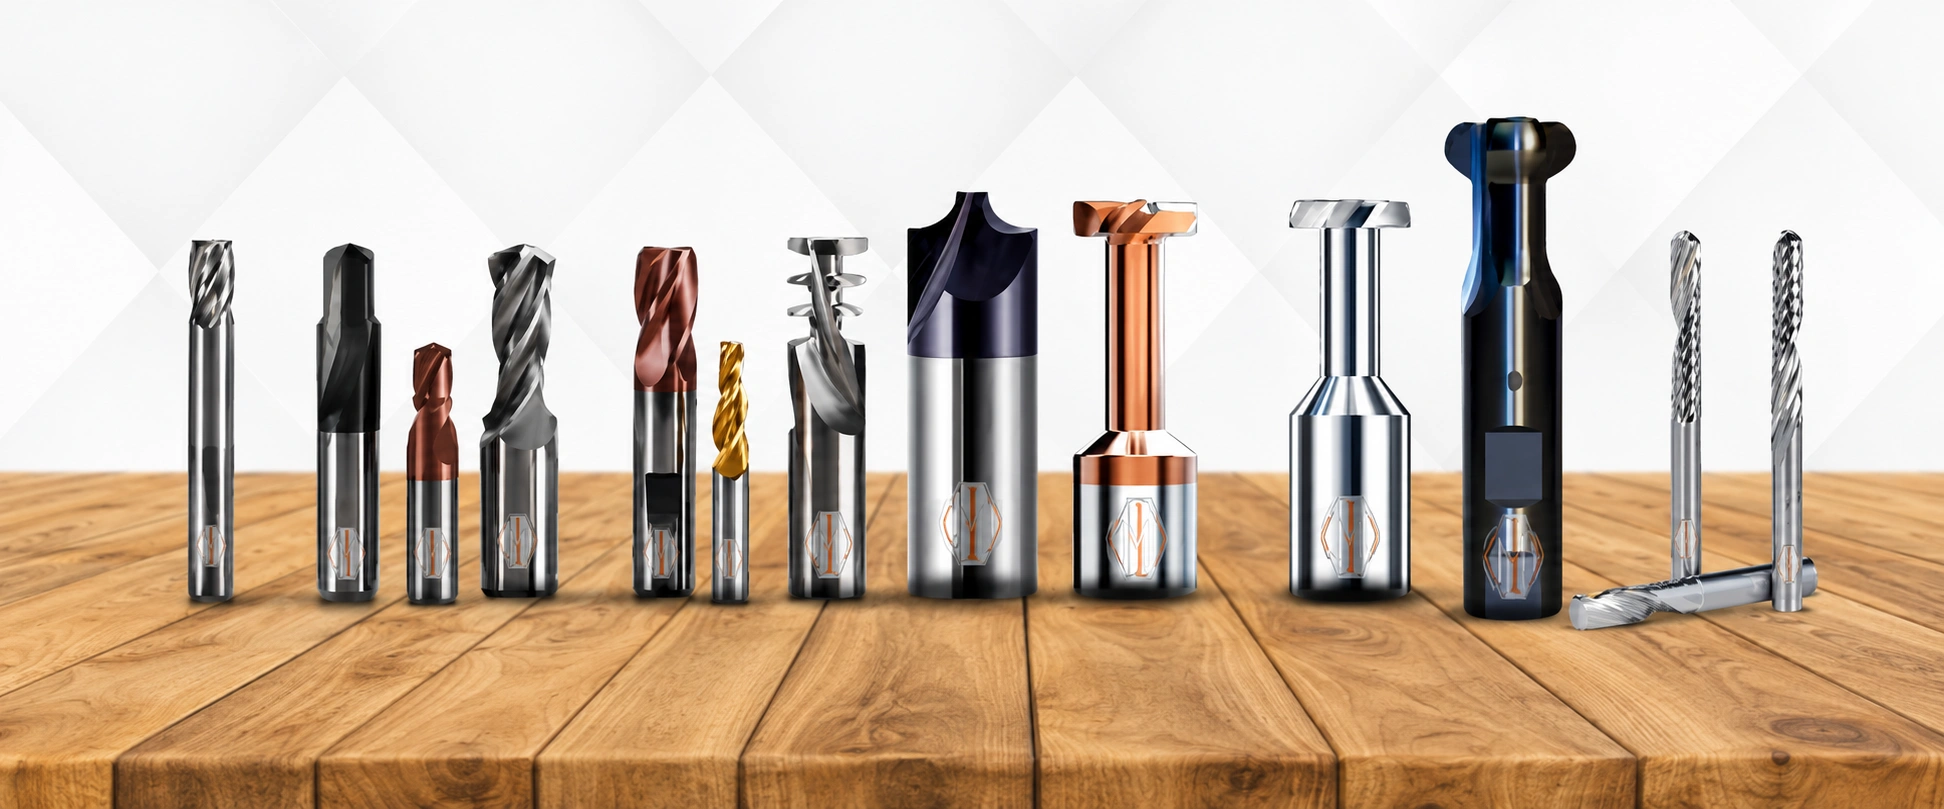
Corner radius, roughing, profile, micro, step, taper, 4 flute and 6 flute end mills, ground on 5-axis CNC for long tool life. Send us your drawing for a custom end mill.
General-purpose end mills for slotting, pocketing, profiling and finishing in steel, stainless steel, cast iron and aluminium.
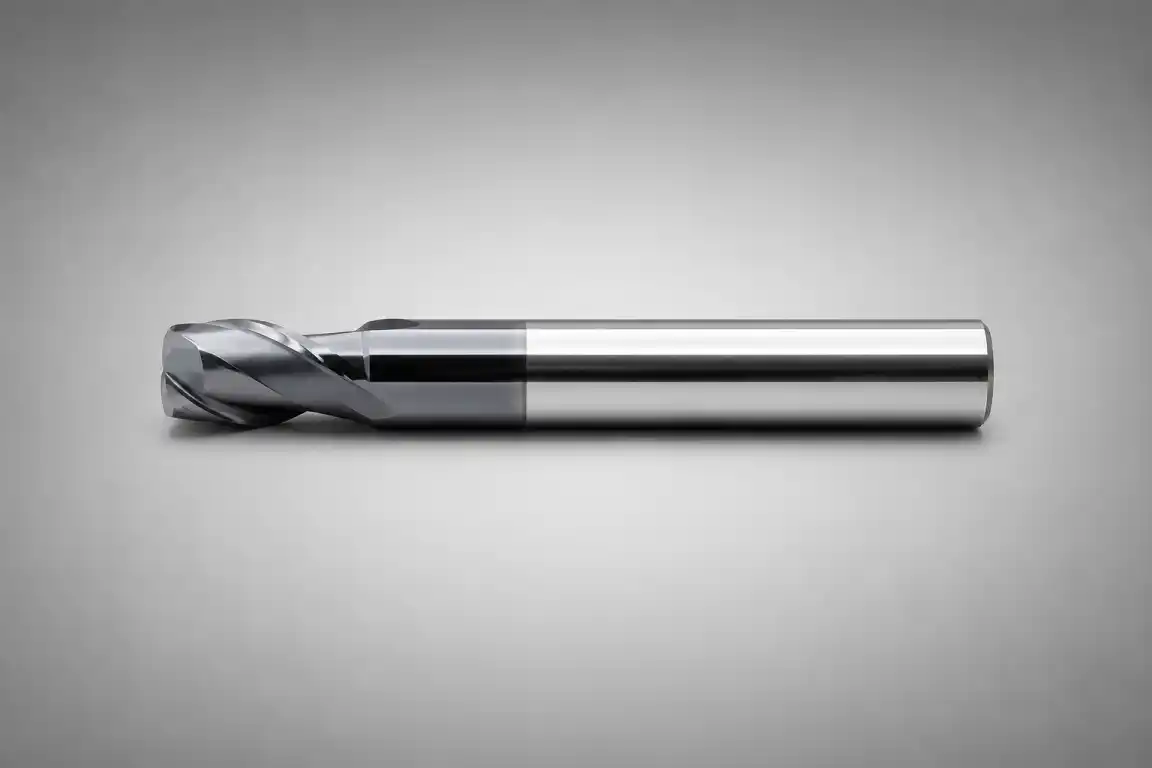
A radius on the cutting corner spreads the load, reduces chipping and leaves a rounded internal corner in one pass.
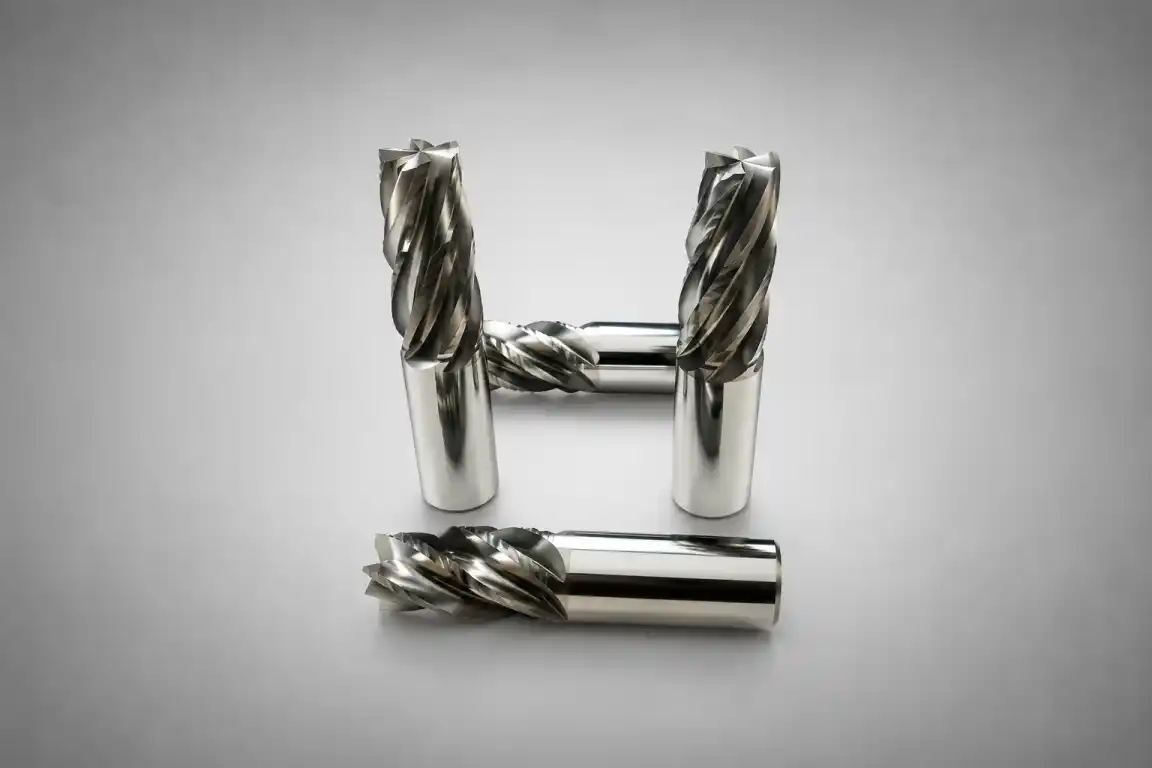
Ground to the contour, radius or chamfer of your part, so one tool does the work of several passes. Made to your drawing.
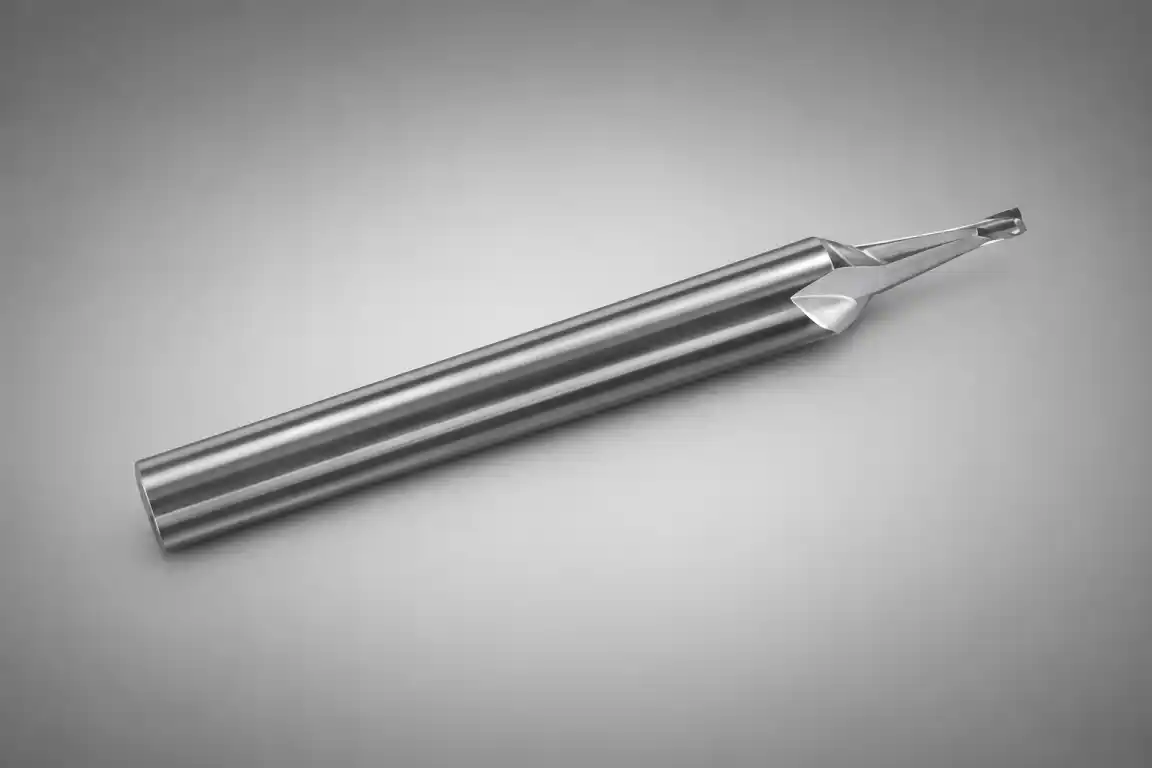
Small-diameter end mills for fine detail, miniature components, watch parts and intricate mould features.
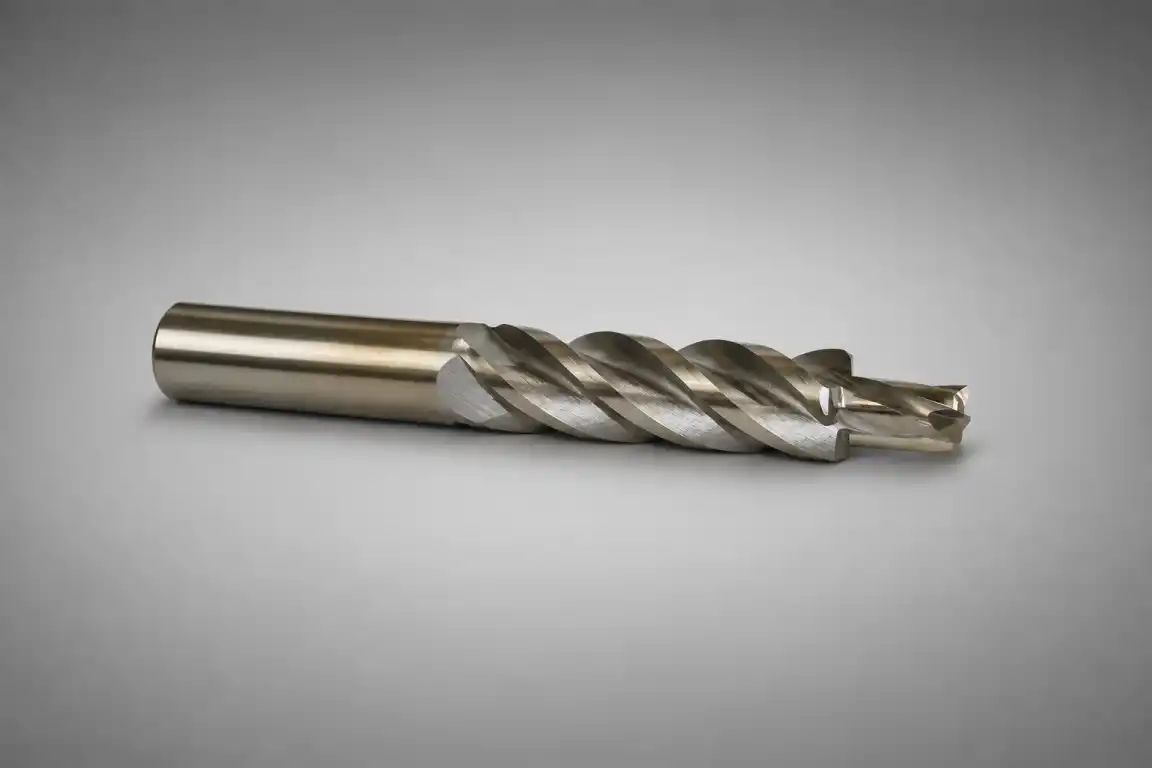
Cut two or more diameters, or a step and shoulder, in one pass. Fewer tool changes and a shorter cycle time.
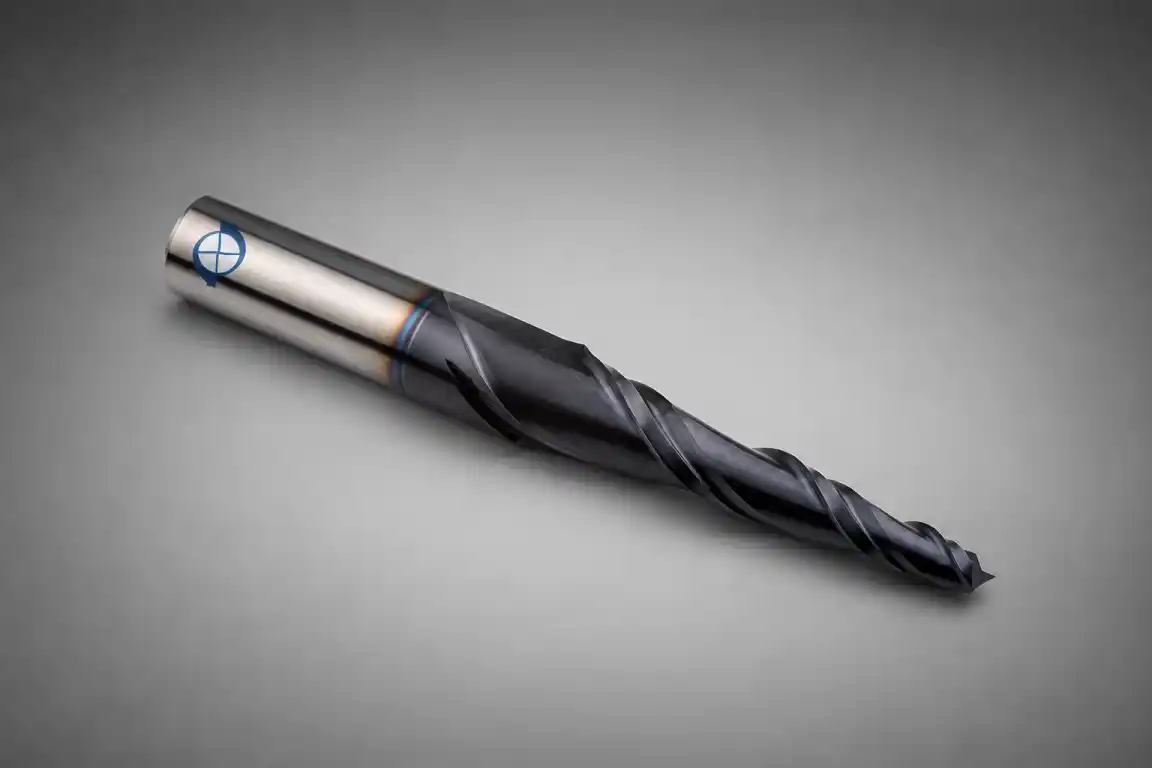
For angled walls, draft angles and deep cavities in moulds and dies, and for precision profile milling.
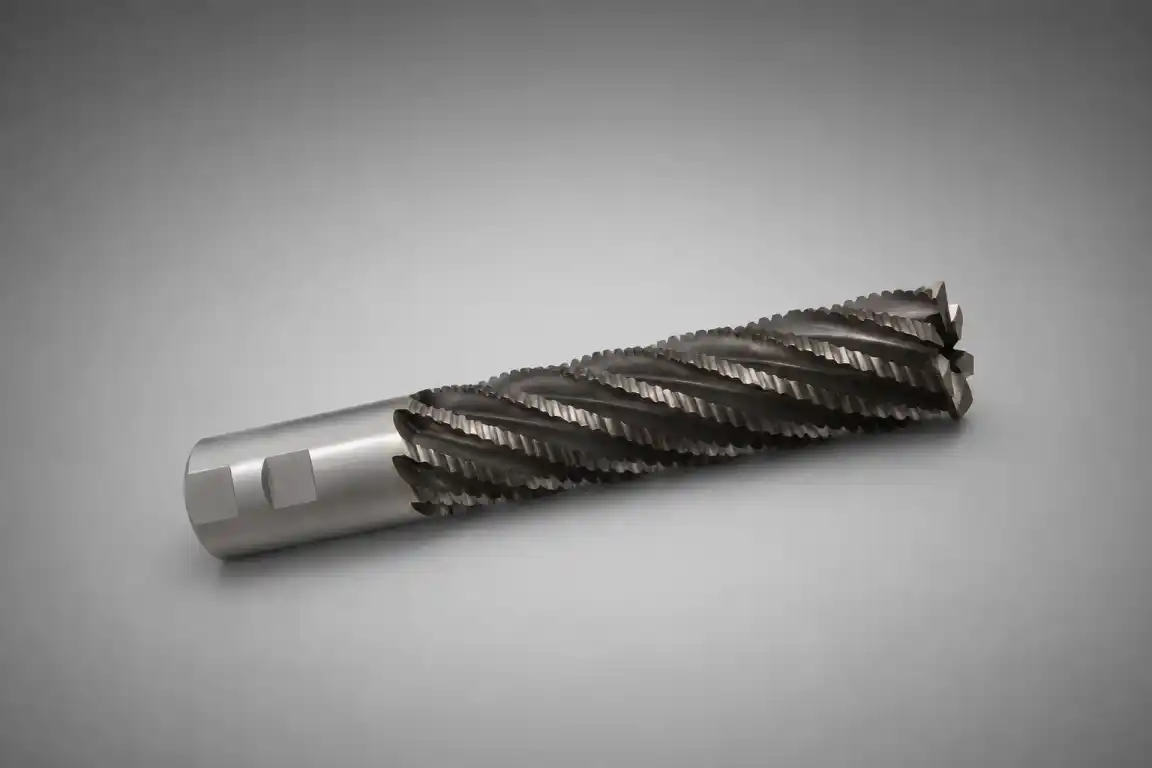
Serrated flutes break chips into small pieces, so you remove more stock at a lower cutting load.
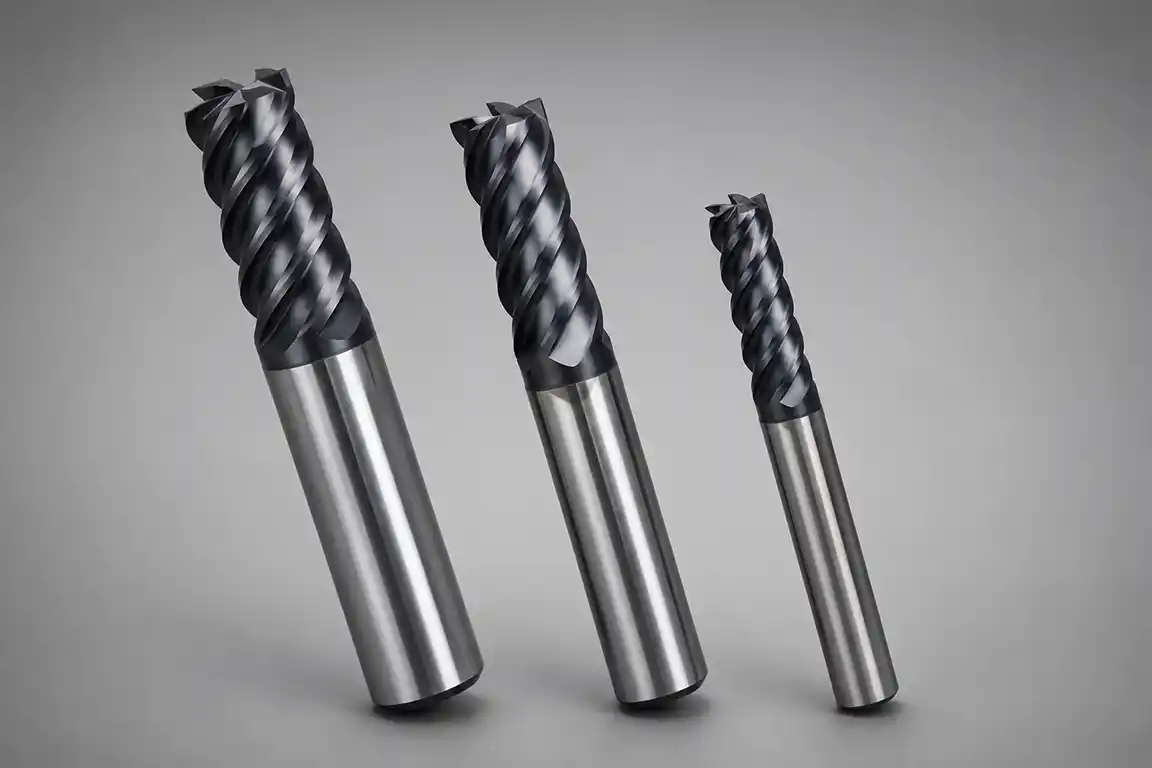
More flutes give a finer finish at higher feed rates. Best for light finishing cuts in harder steels.
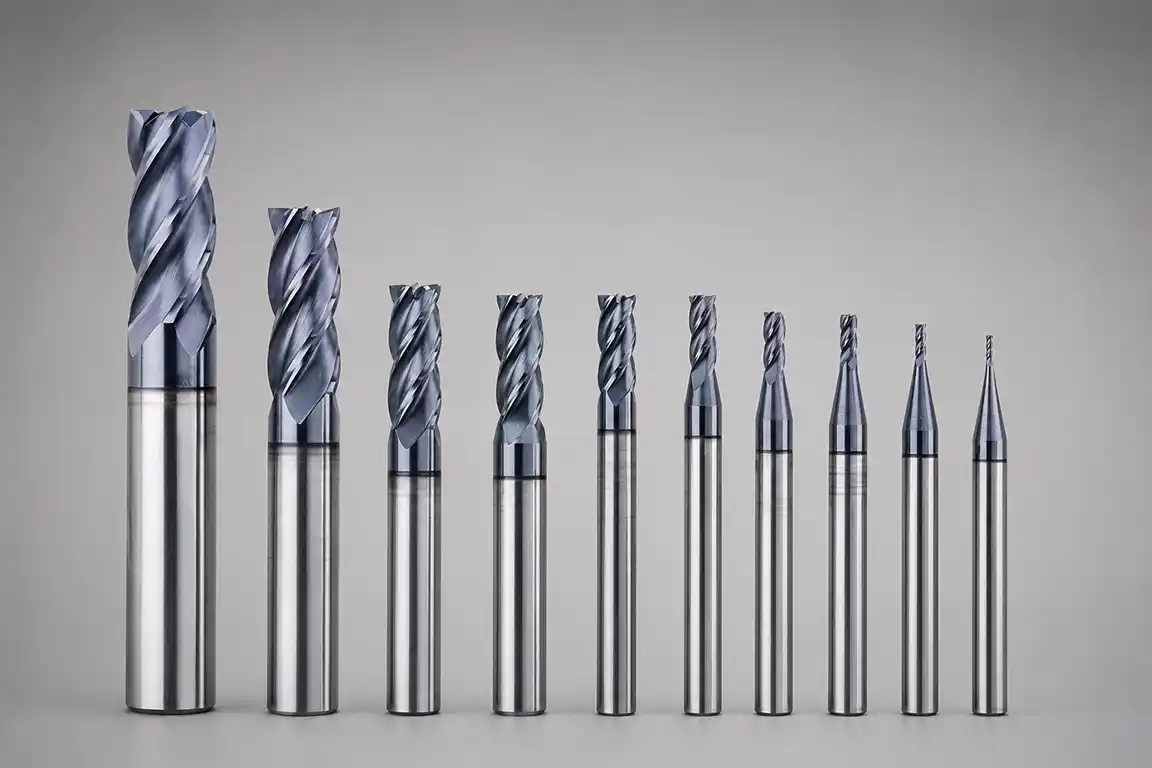
Balanced rigidity and chip space. The everyday choice for steels and stainless steel on CNC and VMC machines.
Share the end mill type, size and what you are machining. We reply with a price.
A quote is quicker when you mention end mill type, diameter, flute count and length, shank, work material, coating and quantity. Add a drawing or worn sample if you have one.
Find the operation on your drawing, then read across to the end mill that suits it.
| Operation | Recommended end mill | Why |
|---|---|---|
| Slotting, pocketing, general profiling | 4 flute end mills | Clean material removal with good chip clearance in steel and stainless steel |
| Heavy stock removal | Roughing end mills | Serrated flutes break chips and lower the cutting load |
| Fine finishing in harder steels | 6 flute end mills | Finer surface finish at higher feed rates |
| Strong corners, rounded internal corners | Corner radius end mills | Less edge chipping and longer tool life |
| Contours, radii and chamfers to drawing | Profile end mills | The same shape on every part in fewer passes |
| Fine detail and small features | Micro end mills | Accurate cutting at very small diameters |
| Two diameters or a step in one pass | Step end mills | Fewer tool changes and a shorter cycle |
| Angled walls and deep cavities | Taper end mills | Draft angles in moulds and dies |
| 3D die and mould surfaces | Ball nose end mills | Smooth contours with fewer visible scallops |
Tell us the material, the operation and the diameter. We reply with a suggested end mill and a price.
Flute count and work material narrow the choice quickly.
| Flutes | Best for | What to know |
|---|---|---|
| Fewer flutes | Aluminium and other soft, sticky metals | More room for chips, so the flutes are less likely to clog. |
| 4 flutes | Steel, alloy steel and stainless steel | A balance of rigidity and chip space for slotting, profiling and roughing. |
| 6 flutes | Light finishing cuts in harder steels | A finer finish at higher feed rates. There is less room for chips, so keep the cuts light. |
Treat this as a starting point. Your machine, holder and depth of cut will move the right answer.
A 4 flute end mill handles most slotting and profiling. Use a corner radius end mill where the edge takes heavy loads, and a roughing end mill to remove stock before finishing.
Stainless hardens under the cut if the end mill rubs. Keep a constant chip load, avoid dwelling at corners, and hold the tool in a rigid, low-runout holder with coolant on the edge.
Use light radial cuts, a rigid holder and low runout. A 6 flute or corner radius end mill gives a fine finish and a stronger edge.
Aluminium welds to the edge and packs the flutes. Pick fewer flutes with generous flute space, and use coolant or an air blast to carry chips away.
Ordering from the manufacturer gets you a straight answer on flutes, coating and lead time. Longer edge life is what brings the cost per part down.
Premium German carbide holds a sharp edge through long runs in steel, stainless steel and cast iron, which means fewer stops to change worn end mills.
Flute form, core and corner geometry are ground on 5-axis CNC machines and checked before dispatch, so offsets stay put when you swap in a fresh end mill.
Need a radius, chamfer, step or taper cut in one pass? Send a drawing or a worn sample and we quote an end mill ground for that feature.
Ask about flute count, shank and lead time from the team that grinds the tool, not a middleman.
End mills for machine shops across India, from one manufacturer.
Share the end mill type, diameter and material by call, WhatsApp or the quote form. We confirm the price and the delivery time for your location, and overseas buyers can enquire for export on the same channels.
Straight answers on flutes, sizes, coatings and ordering.
An end mill is a milling cutter that cuts on its end face and along its sides. CNC and VMC machines use it for slotting, pocketing, profiling, contouring and finishing. Solid carbide versions are tungsten carbide throughout, which allows higher speeds and a longer edge life than HSS.
Mastertech Business Solutions Pvt. Ltd. grinds solid carbide end mills at MIDC Bhosari, Pune. Standard types and special profiles are made in-house and sold direct to factories and machine shops.
We make solid carbide end mills, corner radius, profile, micro, step, taper and roughing end mills, 4 flute and 6 flute end mills, and ball nose end mills. Special end mills are made to your drawing or sample.
Fewer flutes leave more room for chips, which suits aluminium and other soft metals. Four flutes suit steels and stainless steel. Six flutes are used for light finishing cuts in harder steels, where a finer finish matters more than chip space. Tell us your material and operation and we will suggest the right one.
A square end mill has a sharp corner, which is the most exposed part of the edge and can chip. A corner radius end mill rounds that corner, which makes the edge stronger, extends tool life and leaves a radius in the internal corner of the part.
The usual causes are high runout, long tool stick-out, the wrong chip load, dwelling or rubbing in stainless steel, and poor chip evacuation. Carbide resists wear but not shock, so keep the tool short in a rigid holder and run the recommended chip load.
Yes. A custom end mill makes sense when one feature would otherwise need two or more tools or setups. Share a drawing or worn sample with the work material and quantity, and we price it.
Yes. We dispatch solid carbide end mills to customers all over India. Give us your delivery location with the requirement and we confirm the price and lead time.
Yes. Export enquiries are welcome. Tell us the end mill type, diameter, flute count, quantity and destination country, and we reply with a quotation.
Send the end mill type, diameter, flute count, flute length, overall length, shank diameter, any coating requirement, the material to be machined and the quantity. A drawing or a worn sample makes the quote faster and more accurate.
More cutting tools ground at the same plant.
Send us your machining requirement or drawing. Mastertech provides precision end mills and CNC cutting tools with the right tool recommendation, competitive pricing, and reliable delivery across India.
Plot No. W-238, J Block, MIDC Bhosari, Anandrao Lande Road, Pune 411026, Maharashtra, India
Tell us the end mill and the job, and we will send you a price.
Get a Quote Call +91 9850073333 WhatsApp Us Email Us